From design to production
DFM review, engineering polymer selection, tooling coordination, sampling and an agreed inspection plan — followed by a controlled launch into series production.
Discuss a new part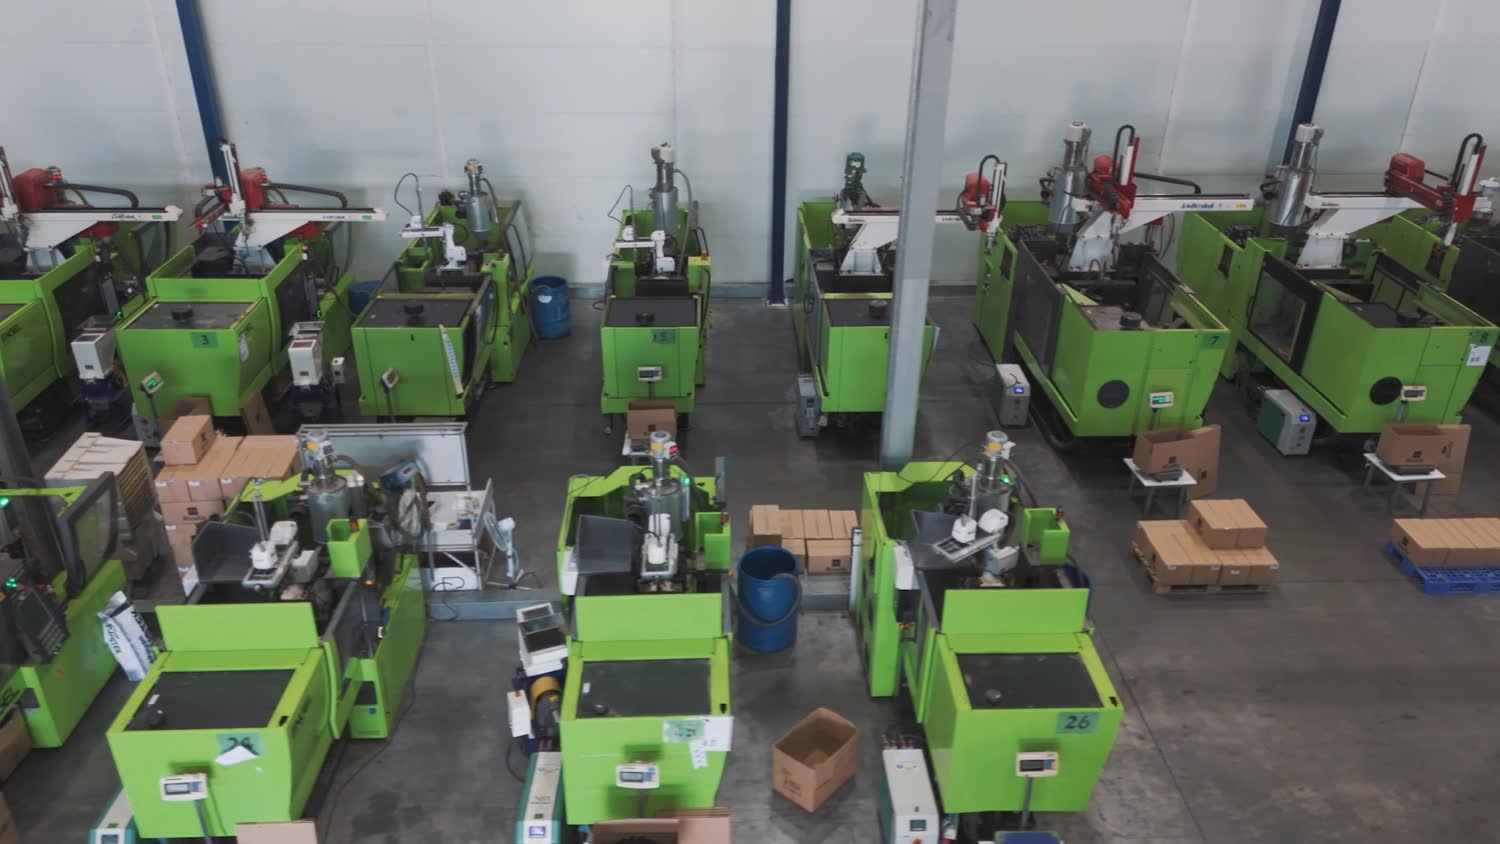
Precision-molded components for UAV and defense programs. We help launch new parts, transfer existing molds and ramp up production — supported by engineering polymers, robotic handling, on-site tooling support and ISO 9001-certified quality management.
Two practical routes: industrialize a new part or move an existing mold into a controlled production process. We can also help when you need additional capacity or an alternative manufacturing partner.
DFM review, engineering polymer selection, tooling coordination, sampling and an agreed inspection plan — followed by a controlled launch into series production.
Discuss a new partTool-condition review, machine compatibility, trial runs, process setup and inspection planning to reduce transfer risk and prepare for the required output.
Discuss a mold transfer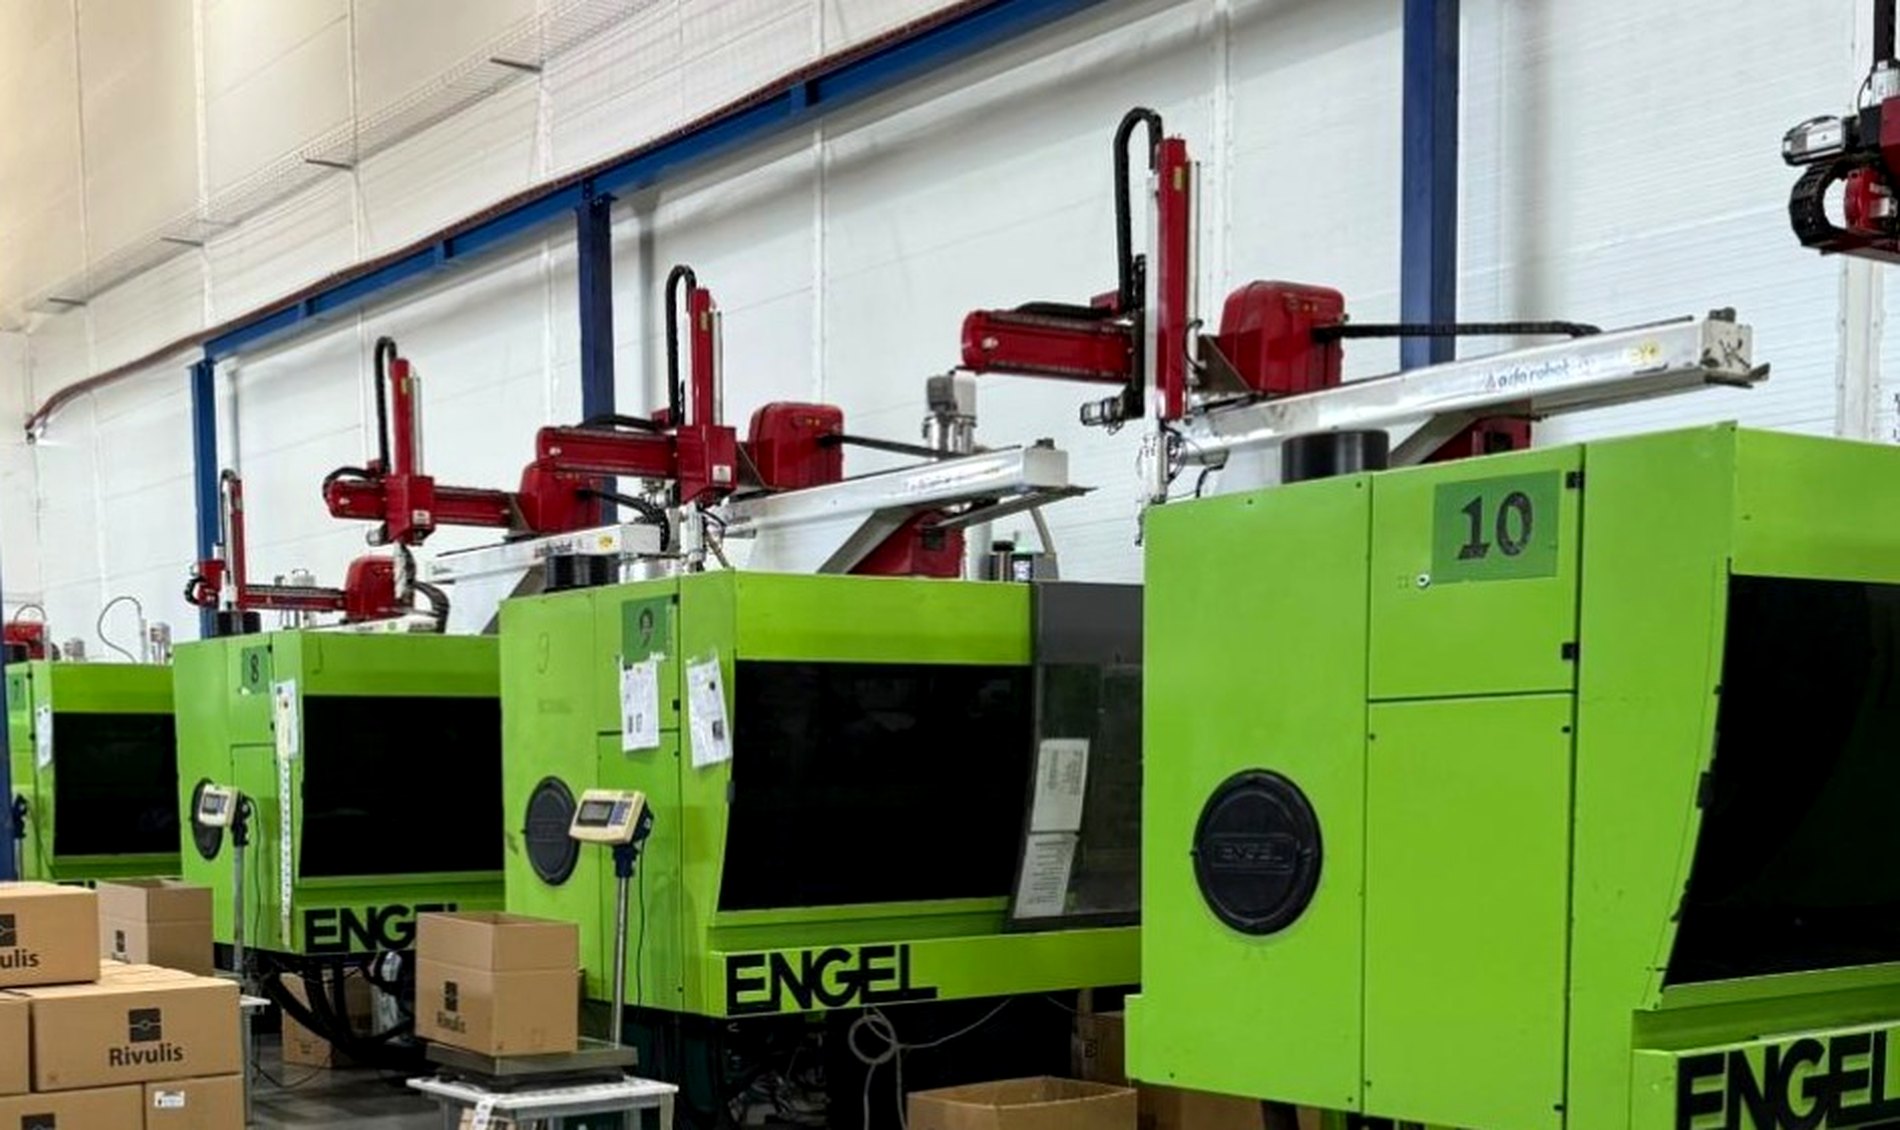
Robotic part removal reduces manual handling and supports repeatable cycles, consistent part presentation and efficient production across shifts.
Before committing to tooling or transferring a mold, we look at the factors that govern repeatability: part geometry, material behavior, mold condition, process setup and inspection requirements.
 Engineering review before production
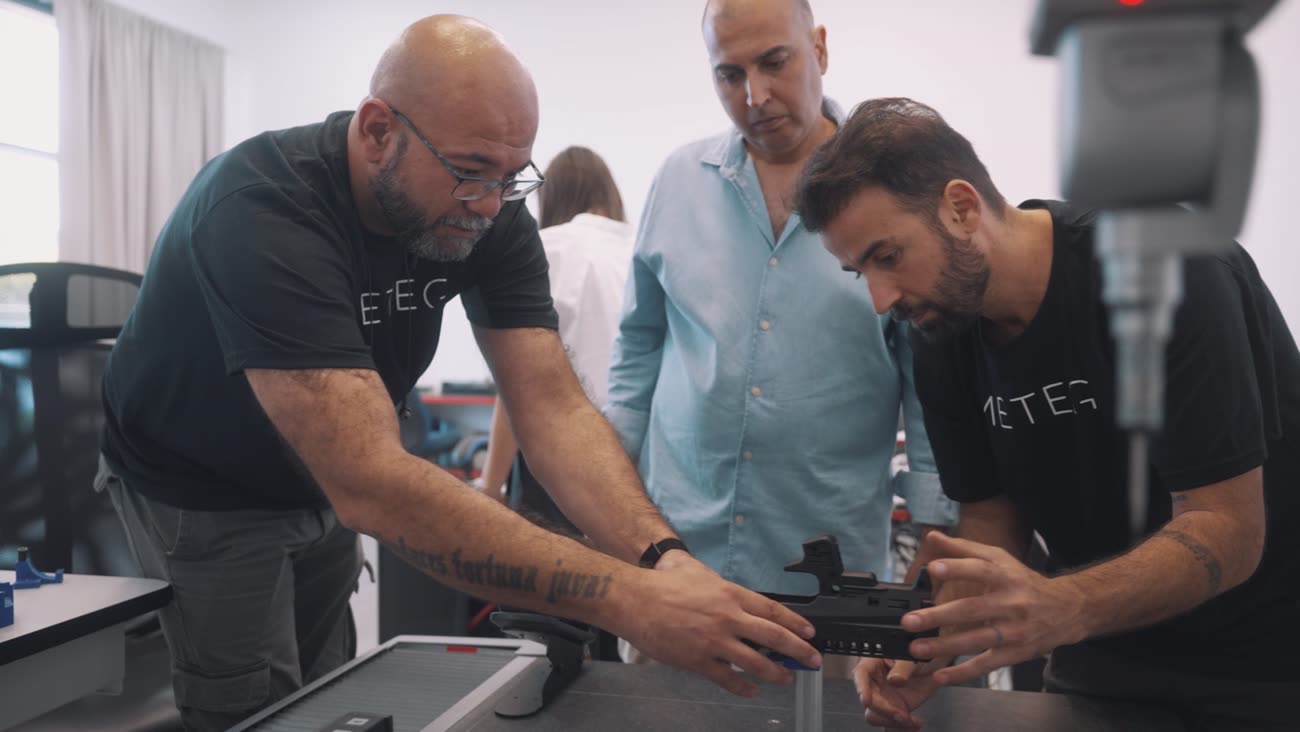
We assess wall thickness, draft angles, shrinkage, warpage, gate locations and sink risks, with recommendations aimed at manufacturability, repeatability and cost.
We process engineering polymers, including glass-filled and modified grades. Material selection considers stiffness, strength, temperature, dimensional stability, weight and processing behavior.
For new tools, we evaluate maintainability and possible insert changes. For existing molds, we review condition and compatibility before committing to a transfer or modification.
Machine selection, process parameters, automated part handling, inspection and packing are planned around the actual part and required volumes, not just a successful first sample.
Approximately 40 presses across a wide clamping-force range support diverse molding requirements, from small technical parts to larger housings. Production capacity, automated handling and experienced process teams help us support repeatable output as volumes grow.
Shot weight refers to the material injected per cycle; it is not necessarily the weight of a single finished part.
We match clamping force, shot capacity, tooling and process settings to the application. The right machine and stable process matter for dimensional consistency and efficient production.
Engineering polymers require disciplined drying, material handling and mold-temperature control. Dedicated ancillary equipment supports predictable processing across production runs.
Depending on the program, inspection, functional testing, subassembly and packing can be integrated into the production scope and delivery specification.
 Small parts, same floor
A capable press is only the starting point. Setup discipline, material preparation and in-process checks are essential to stable molding.
Our experienced setters and process technicians establish molding parameters, monitor variation and troubleshoot issues during production, transfer and ramp-up.
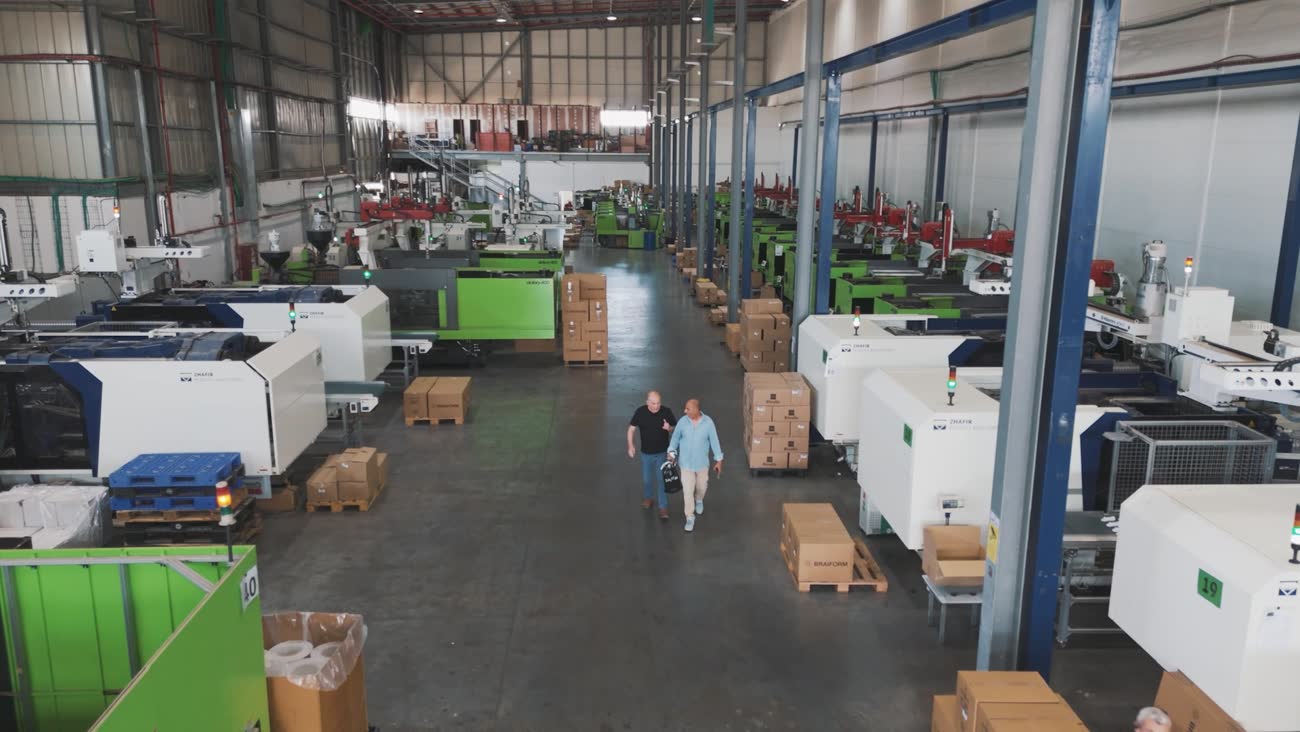
It takes more than a capable press to keep a program running. Our tooling and production teams work closely on maintenance, troubleshooting and corrective action to restore a stable process and minimize avoidable downtime.
Molds require regular care. Wear, contamination, damage and dimensional drift can affect part quality, cycle stability and delivery schedules.
Our tooling capabilities include routine maintenance, ultrasonic cleaning, troubleshooting and mold repairs. We coordinate technical decisions close to the production floor and agree corrective work with the customer.
The scope and timing of corrective work depend on tool condition and project requirements. The aim is to restore a stable process and avoid repeated disruption.
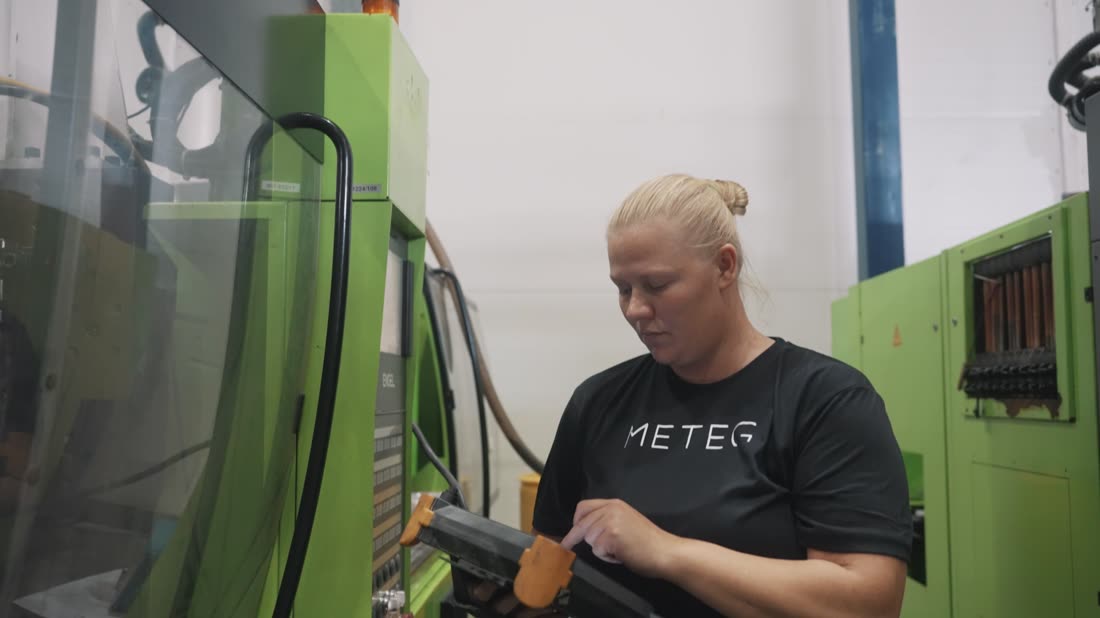 Tooling support close to production
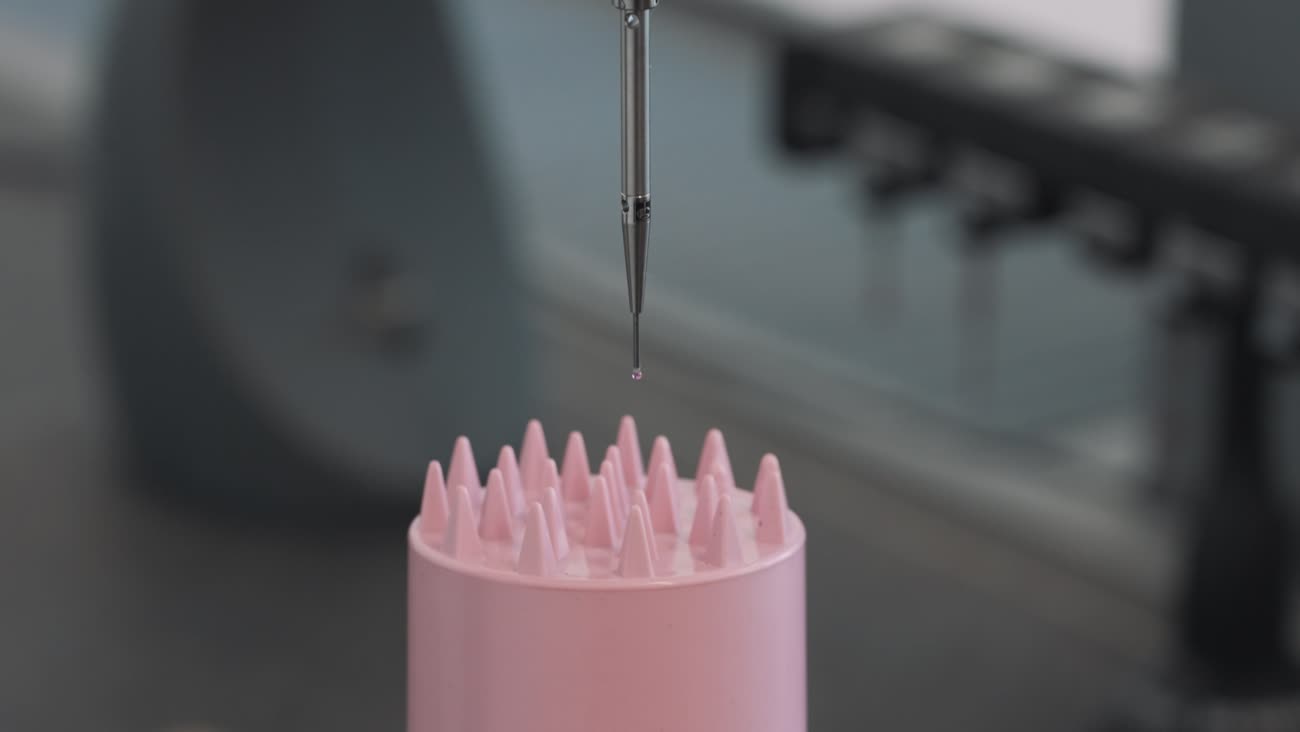 Dimensional inspection
We verify critical dimensions against agreed drawings and acceptance criteria. First-article inspection, in-process sampling, functional checks and water-pressure testing can be included where relevant, with records aligned to the approved inspection plan.
Testing methods, sample frequency and documentation are defined with the customer before release. We do not assume every part or program needs the same inspection package.
Founded in 1983, Meteg Plast operates in the Sapirim Industrial Park, Sha'ar HaNegev, Israel. We have produced technical molded parts for defense, medical, electronics, irrigation and other industrial applications.
We already manufacture molded components for customers in Israel's defense sector. We treat technical information, acceptance criteria and project communication as matters to define clearly before production begins.
Local manufacturing, direct engineering communication and mold support near the machines help reduce handoffs. Tool custody and program-specific information-handling requirements are agreed with the customer.
Tell us whether you need a new mold, production transfer or additional capacity. Share material, target volumes, timing and drawing requirements; an NDA can be arranged before sensitive information is exchanged.
We assess part geometry or existing tooling, engineering material, machine fit, inspection requirements and production risks. We then agree the scope needed for a quotation.
We coordinate new tooling when needed, or review and trial an existing mold. Tool condition, process setup and modifications are evaluated before release.
We evaluate sample parts against agreed specifications, with dimensional, functional or other testing as the approved project plan requires.
Production scheduling, robotic handling, in-process inspection and optional packing or assembly are coordinated to meet confirmed volumes. Additional capacity is planned as demand increases.
New component, existing mold or a production bottleneck? Tell us the tooling status, target volumes and timing. We will review the requirements and discuss the next steps in English or Hebrew.
For confidential projects, request an NDA before sharing drawings or controlled technical information.